Why Cold Drawing Creates Superior Dimensional Accuracy
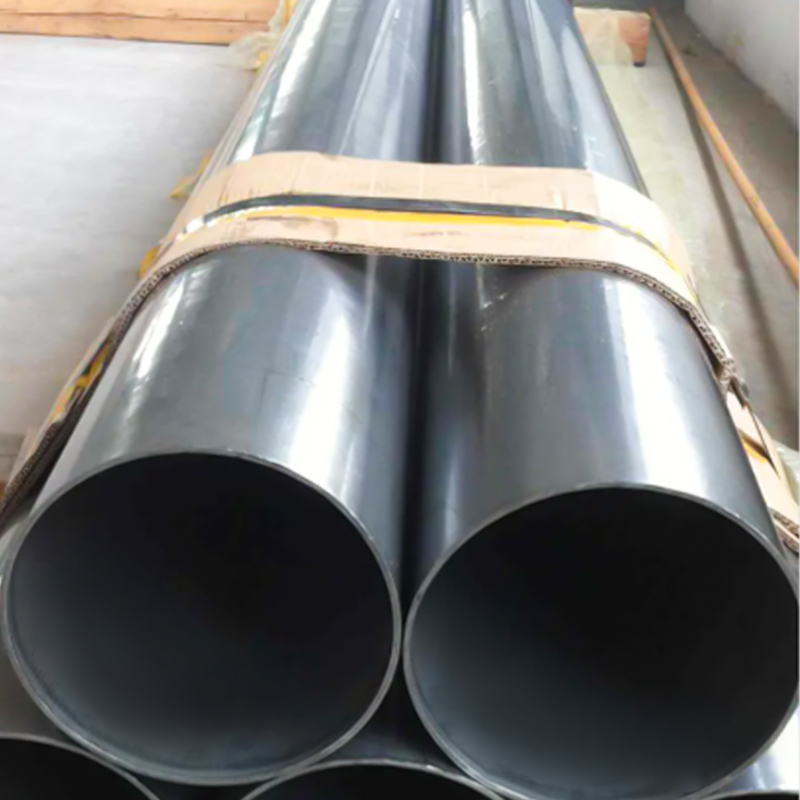
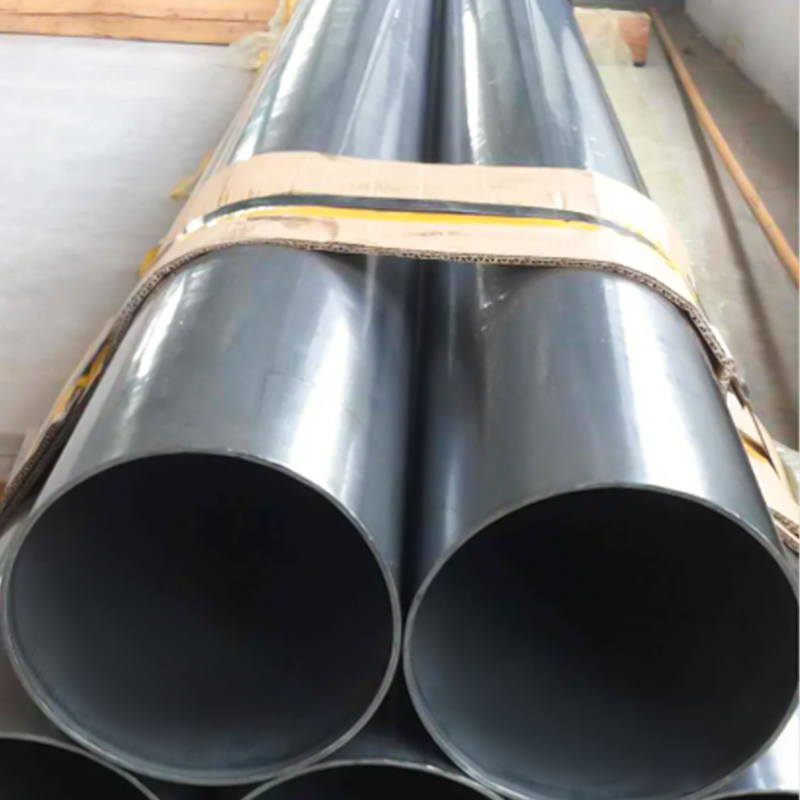
Cold drawing compresses the cold-rolled steel tube through precision dies at room temperature, fundamentally altering its microstructure. This process reduces grain size and work-hardens the material, delivering tolerances as tight as ±0.05mm on outer diameter and ±0.02mm on wall thickness—far exceeding hot-finished alternatives.
The absence of thermal distortion means the tube retains dimensional stability throughout its length. For applications like hydraulic cylinders or precision mechanical assemblies where concentricity and straightness are non-negotiable, cold drawing is the only viable manufacturing route. Our multi-pass drawing sequences, combined with real-time dimensional monitoring systems, ensure every tube leaving our facility meets aerospace-grade geometric specifications.
Heat Treatment Sequences That Define Performance Characteristics
Post-draw heat treatment is where mechanical properties are engineered to specification. The choice between stress relieving, normalizing, or full annealing determines whether your tube optimizes for machinability, strength, or dimensional stability.
Common Heat Treatment Routes:
- Stress Relieving (550-650°C): Removes residual stresses from cold working while maintaining high strength; ideal for components subject to welding or further machining
- Normalizing (880-920°C): Refines grain structure and homogenizes properties; balances strength and ductility for general structural applications
- Full Annealing (720-780°C): Maximizes machinability and formability by creating a soft, uniform microstructure; recommended when extensive secondary operations are planned
We maintain fully automated heat treatment furnaces with ±5°C temperature control and controlled atmosphere environments to prevent surface decarburization—a critical detail that separates premium tubes from commodity products.
Surface Finish Impact on Hydraulic System Efficiency
In hydraulic applications, internal surface roughness directly governs seal life and system efficiency. A rough bore accelerates seal wear, generates particle contamination, and increases pressure drop across the circuit.
Cold-drawn tubes achieve Ra 0.4-0.8μm internal finish as-produced, eliminating the need for costly honing operations in many applications. For ultra-precision hydraulic cylinders operating above 350 bar, we offer burnishing and honing services that reduce surface roughness to Ra 0.2μm or better, extending seal life by 300-500% compared to standard commercial tubing.
External surface treatments—phosphating for corrosion resistance, chrome plating for wear resistance, or electropolishing for cleanroom compatibility—are applied using our in-house finishing lines, ensuring complete supply chain control and traceability.
Material Selection Beyond Generic Steel Grades
Specifying "carbon steel tube" is insufficient for engineered applications. The carbon content, alloying elements, and inclusion control define whether your component succeeds or fails in service.
Critical Material Considerations:
- Low-carbon grades (C10, C15): Superior weldability and cold formability; suitable for brackets, spacers, and non-critical structures
- Medium-carbon grades (C45, 4140): Heat-treatable to 800+ MPa tensile strength; the workhorse for hydraulic cylinders, shafts, and high-stress components
- Alloy steels (4130, 4340): Enhanced hardenability and fatigue resistance through chromium-molybdenum additions; required for aerospace and automotive critical applications
Our metallurgical laboratory performs spectroscopic analysis on every heat lot, with full traceability documentation linking finished tubes back to raw material certificates—a requirement for industries operating under AS9100 or IATF 16949 quality systems.
Non-Destructive Testing Protocols for Mission-Critical Components
Visual inspection catches surface defects, but subsurface discontinuities—laminations, seams, or inclusions—require advanced NDT methods. For tubes destined for high-pressure or safety-critical service, the following tests are essential:
- Eddy Current Testing: Detects surface and near-surface cracks with sensitivity down to 0.1mm depth; standard for hydraulic tubes operating above 250 bar
- Ultrasonic Testing: Identifies internal voids, laminations, and wall thickness variations throughout the tube body; mandatory for ASME pressure vessel components
- Hydrostatic Pressure Testing: Proof-loads tubes to 1.5-2× working pressure to verify structural integrity; eliminates marginal parts before they reach your production line
Our automated NDT systems inspect 100% of production at line speed, with automatic rejection of non-conforming material. Test records are digitally archived and available for customer audit—because in regulated industries, documentation is as important as the product itself.
Tube End Preparation Strategies for Assembly Efficiency
How you finish tube ends dramatically affects downstream assembly costs. A poorly prepared end means extra handling, rework, and potential rejection during welding or brazing operations.
Chamfering removes sharp edges that damage seals or O-rings during insertion, while facing ensures perpendicularity for leak-free connections. For hydraulic fittings, a 15-30° chamfer is standard; for welded assemblies, square-cut ends with ±1° perpendicularity tolerance prevent fit-up gaps.
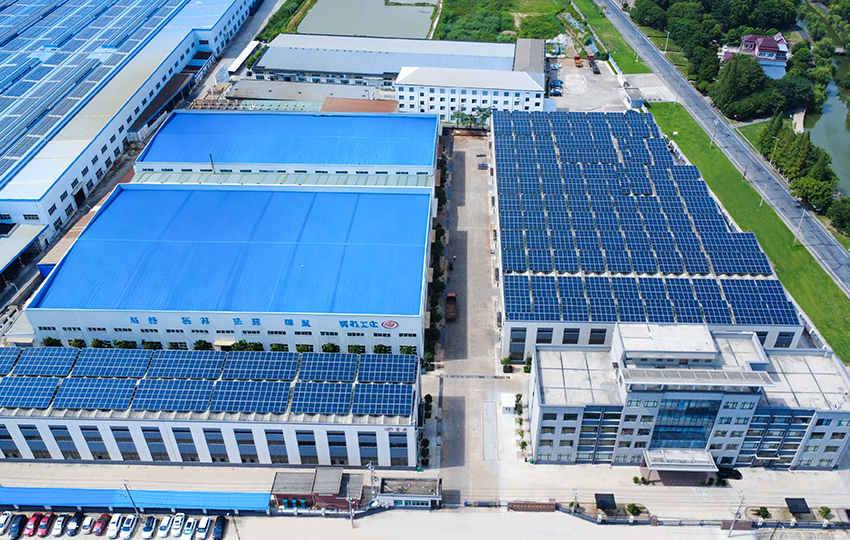
We offer precision end machining as a value-added service, delivering cold-rolled steel tubes that drop directly into your assembly fixtures without secondary operations. This is particularly valuable in high-mix, low-volume manufacturing environments where setup time drives unit costs. With our flexible production systems and over 50,000 tons annual capacity, we handle everything from prototype runs to full-scale production without compromising lead times.
Environmental Compliance in Steel Tube Manufacturing
Global supply chains now demand environmental accountability. RoHS compliance eliminates hazardous substances, while ISO 14001 certification ensures systematic environmental management across production operations.
Cold drawing is inherently more sustainable than hot-forming processes: no combustion emissions, 60% lower energy consumption per ton, and minimal material waste due to precision sizing. Our closed-loop coolant recycling systems and waste oil recovery programs further reduce environmental impact.
For customers targeting carbon-neutral supply chains, we provide product carbon footprint data and third-party verified environmental declarations. As regulatory pressure intensifies—particularly in European and North American markets—partnering with environmentally compliant manufacturers isn't optional; it's a competitive necessity.